Way Lubricants vs Spindle Oils: Precision Machine Tool Chemistry
A precision CNC machine tool runs two entirely different lubrication regimes within a few feet of each other, and confusing them is one of the more expensive mistakes a maintenance team can make. The debate over way lubricant vs spindle oil is not a question of which is "better" — it's a question of two opposite engineering problems that happen to sit on the same machine bed. A slide way needs to hold onto oil against gravity while eliminating the jerky stick-slip motion that ruins fine surface finish; a spindle bearing needs to shed oil freely at rotational speeds where any resistance to flow shows up immediately as heat. This guide breaks down the tackifier chemistry that defines way lubricants, the low-viscosity design logic behind spindle oils, why the two formulations can never substitute for each other, and how to select the correct product for each lubrication point on a machine tool. It complements our detailed guide to slide way oil formulation for CNC machines.
One Machine, Two Completely Different Friction Problems
Every precision machine tool has at least two distinct categories of moving contact that need lubrication, and treating them as a single "machine oil" problem is where selection mistakes start. A sliding guideway experiences intermittent, low-speed, often reversing motion under significant static load — the carriage stops, holds position, then moves again, sometimes at feed rates measured in millimeters per minute. A spindle bearing, by contrast, experiences continuous, high-speed rotation, often tens of thousands of revolutions per minute in modern machining centers, with the lubricant's job being almost entirely about heat management rather than static friction.
These two friction regimes demand opposite properties from the lubricant film:
- Way surfaces — need a film that resists drainage under gravity, bridges the transition from static to kinetic friction smoothly, and survives long dwell periods without thinning out
- Spindle bearings — need a film thin enough to avoid viscous drag and churning losses at high rotational speed, prioritizing heat rejection and low power consumption over static adhesion
A machine tool builder's lubrication chart reflects this split explicitly, specifying a different product — often from a different viscosity family entirely — for each type of point. Understanding why starts with looking at what way lubricant chemistry is actually solving for.
Way Lubricant Vs Spindle Oil: What Way Oil Is Built For
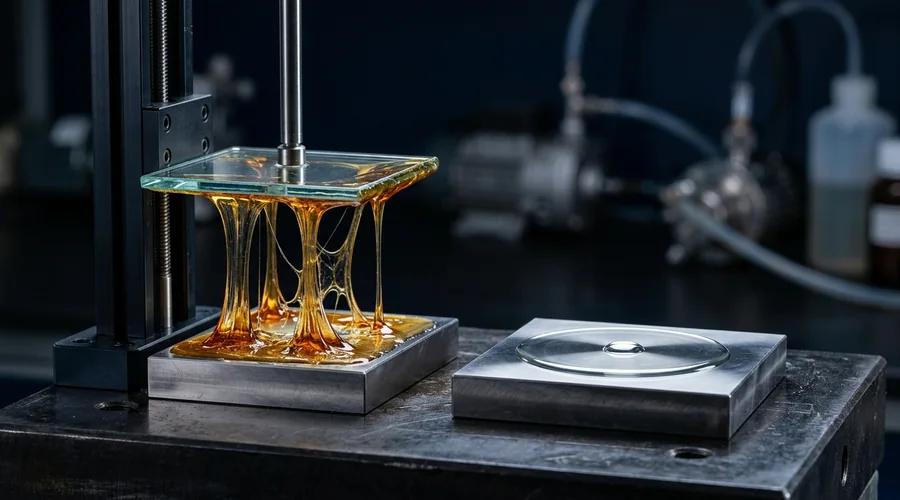
Way lubricant exists to solve a problem spindle oil never encounters: staying where you put it. A machine tool guideway can be vertical, inclined, or horizontal depending on the axis, and the lubricant film has to remain adherent across all of those orientations between lubrication cycles, sometimes for hours. The formulation strategy for achieving this centers on a tackifier additive, most commonly polyisobutylene, which increases the oil's resistance to being drained or flung off a surface without proportionally raising its bulk viscosity — a property covered in depth in our dedicated guide to way oil formulation for CNC machines.
The functional requirements a way lubricant has to satisfy:
- Anti-stick-slip performance — friction modifiers that smooth the transition between static and kinetic friction coefficients, preventing the jerky motion that degrades surface finish and positioning accuracy at low feed rates
- Tackiness and film persistence — the polyisobutylene tackifier keeps the oil adhered to vertical and inclined ways rather than draining away under gravity
- Load-carrying capacity — the way surface carries the static and dynamic weight of the carriage and workpiece, requiring a film that resists being squeezed out under pressure
- Coolant demulsibility — way surfaces are frequently splashed with water-based cutting coolant, so the oil must separate cleanly rather than emulsify and lose its properties
None of these priorities transfer usefully to a spindle bearing, where the lubricant is never asked to resist gravity between cycles and where tackiness would be actively counterproductive. That contrast becomes obvious once you look at what spindle oil is optimized for instead.
Spindle Oil Chemistry: Precision Machine Tool Lubrication at Speed
Spindle oil is formulated around a single dominant constraint: minimizing heat generation inside a bearing spinning at very high speed. Unlike a way surface, a spindle bearing is in continuous relative motion during operation and typically receives a constant, metered oil supply rather than depending on a persistent film to survive idle periods. That changes the formulation priority completely — instead of maximizing adhesion, spindle oil formulation minimizes viscous drag.
The properties that define a spindle oil formulation:
- Low viscosity — typically the lowest viscosity grades used anywhere on the machine, chosen specifically to reduce churning losses and heat generation as bearing speed increases
- Excellent oxidation stability — high rotational speed and the associated heat accelerate oxidative degradation, so spindle oils rely on antioxidant chemistry to maintain a stable viscosity and acid number over long service intervals
- Low foaming tendency — high-speed churning entrains air readily, and foam reduces the oil's effective load-carrying and heat-transfer capacity inside the bearing
- Rust and corrosion protection — precision bearing surfaces are highly sensitive to corrosion pitting, which directly degrades rotational accuracy and bearing life
- Thermal stability with minimal viscosity change — since spindle temperature directly affects thermal growth and therefore dimensional accuracy in precision work, the oil's viscosity-temperature behavior is tightly controlled
With both formulations understood on their own terms, the practical differences become easiest to grasp side by side.
Viscosity, Tackiness and Selection: A Direct Comparison
Putting the two lubricant families in a single table makes the divergence in design philosophy concrete. Every property that makes a way oil effective on a guideway either does nothing for a spindle bearing or actively works against it, and the reverse is equally true — this is a genuine either/or in formulation chemistry, not a spectrum with overlap in the middle.
| Property | Way lubricant | Spindle oil |
|---|---|---|
| Typical ISO VG range | 32 – 220 | 2 – 32 |
| Tackifier (e.g. polyisobutylene) | Essential — core additive | Absent — would increase drag |
| Primary friction regime | Intermittent sliding, static-to-kinetic transition | Continuous high-speed rotation |
| Design priority | Film adhesion, stick-slip elimination | Low drag, heat rejection |
| Gravity drainage resistance needed | Yes — critical on vertical/inclined ways | No — not exposed to standing drainage |
| Typical application method | Metered lubricator to way surface | Oil bath, mist, or jet lubrication in sealed housing |
The table also explains why a machine tool's central lubrication system, when it has one, almost always runs way oil and spindle oil through entirely separate reservoirs and delivery lines rather than a shared supply — mixing them defeats the purpose of both formulations. What happens when someone bypasses that separation, deliberately or by mistake, is worth spelling out clearly.
What Happens If You Use One Lubricant in Place of the Other
Substituting one lubricant type for the other is not a theoretical formulation exercise — it happens in real shops, usually because a maintenance technician grabs whichever drum is closest or a small shop tries to simplify inventory by stocking one general-purpose oil. The consequences show up quickly and are specific to each direction of the mistake.
Using spindle oil on a way surface:
- Film drainage — the low-viscosity oil lacks tackifying chemistry and drains off vertical and inclined ways between lubrication cycles
- Stick-slip onset — the way runs in boundary lubrication once the film thins, producing the jerky motion that degrades surface finish and positioning accuracy
- Accelerated way wear — repeated boundary contact between the carriage and way surface accelerates mechanical wear on both
Using way oil in a spindle bearing:
- Increased churning losses — the higher viscosity and tackiness raise viscous drag at high rotational speed
- Elevated operating temperature — increased drag converts directly to heat, which can accelerate oil oxidation and, in precision spindles, shift thermal growth enough to affect dimensional accuracy
- Reduced speed capability — a spindle rated for a given maximum RPM with the correct low-viscosity oil may not safely reach that speed with a heavier, tackier lubricant in the bearing
Neither substitution causes instant catastrophic failure, which is exactly what makes it a persistent maintenance mistake — the damage accumulates gradually as reduced surface finish quality, shortened bearing life, or unexplained thermal drift, and it's rarely traced back to a lubrication error until someone checks what's actually in the reservoir.
Selecting the Right Lubricant for Each Point on a Machine Tool
Correct lubricant selection on a precision machine tool comes down to following documentation rather than applying general intuition about "machine oil." Every reputable machine tool builder issues a lubrication chart identifying each grease and oil point on the machine, the required ISO VG grade or specific product recommendation, and the lubrication interval. Deviating from that chart, even with a seemingly similar product, introduces risk the builder has already engineered around.
- Start with the machine builder's lubrication chart — it identifies every lubrication point and the exact grade or product specified for that location
- Confirm way oil grade against expected load and orientation — heavier machines and more heavily loaded or steeply inclined ways generally call for higher-viscosity way oil within the builder's approved range
- Confirm spindle oil grade against the bearing's rated speed — higher-speed spindles typically require lower-viscosity oil to control heat generation, per the builder's specification
- Verify coolant compatibility for way oil — check the way oil's demulsibility rating against the specific coolant chemistry in use on that machine
- Never consolidate way oil and spindle oil into a shared reservoir or delivery system — keep separate, correctly labeled containers and delivery lines to prevent cross-contamination or accidental substitution
Getting this right is a documentation and discipline problem more than a chemistry problem — the formulations already exist and are well understood; the failure mode is almost always in application, not in the product itself. A shop that treats way lubricant and spindle oil as genuinely different products, stocked and labeled separately and applied strictly to the builder's specification, avoids the gradual precision loss and premature wear that comes from treating "machine oil" as a single category.
Frequently Asked Questions
What is the core difference between way lubricant and spindle oil?
Way lubricant and spindle oil solve opposite friction problems on the same machine tool, which is why their chemistry pulls in opposite directions. Way lubricant coats a sliding guideway and must resist gravity drainage on vertical and inclined surfaces while eliminating stick-slip between a stationary way and a moving carriage at very low feed rates — it achieves this with a tackifier additive package, typically polyisobutylene, dissolved in a mid-to-high viscosity base oil.
Spindle oil circulates through a high-speed rotating bearing and must minimize churning losses and heat generation at speeds that can exceed tens of thousands of RPM — it achieves this with a low viscosity base oil and no tackifier at all, since tackiness in a spindle bearing would increase drag and raise operating temperature rather than help it.
Can spindle oil be used on machine ways, or way oil in a spindle bearing?
No, and using either in the other's role causes a predictable failure mode rather than a marginal performance loss. Spindle oil applied to a way surface lacks the tackifier chemistry needed to stay adhered to a vertical or inclined guideway, so it drains away under gravity between lubrication cycles, leaving the way running in boundary lubrication and producing stick-slip motion that shows up directly as poor surface finish and positioning error.
Way oil applied to a spindle bearing introduces exactly the problem spindle oil is designed to avoid — its higher viscosity and tackiness increase churning losses and viscous drag at high rotational speed, which raises bearing operating temperature, can accelerate thermal degradation of the oil, and in precision spindles can measurably affect thermal growth and dimensional accuracy. Machine tool builders specify each lubricant for a reason, and the two are not interchangeable even temporarily.
What viscosity grades are typical for way oils versus spindle oils?
Way oils commonly fall in the ISO VG 32 to ISO VG 220 range depending on the machine builder's specification, with heavier machine tools and larger, more heavily loaded ways typically specified at the higher end of that range to maintain film thickness under load. Spindle oils sit in a much narrower and lower band, typically ISO VG 2 to ISO VG 32, chosen specifically to minimize viscous drag and heat generation at high rotational speeds.
The lower the viscosity, generally the higher the speed capability of the bearing, though this must be balanced against maintaining an adequate lubricant film to prevent metal-to-metal contact. A machine tool builder's lubrication chart will specify the exact ISO VG grade for each lubrication point, and matching that specification takes priority over any general rule of thumb.
What is the tackifier in way lubricant and why doesn't spindle oil use it?
The tackifier in most way lubricant formulations is polyisobutylene, a high-molecular-weight polymer that dramatically increases the oil's resistance to being flung or drained off a surface without proportionally increasing its bulk viscosity at low shear rates. This lets the way oil form a persistent, adherent film on a vertical or inclined guideway that resists gravity for hours, which is exactly what a stationary way needs between lubrication cycles.
Spindle oil never uses this chemistry because a spindle bearing is fully immersed in or continuously fed with oil during operation — it doesn't need a film to survive gravity between cycles — and adding a tackifier would only increase the oil's resistance to flow through the tight clearances of a high-speed bearing, working directly against the low-drag, low-heat-generation goal that spindle oil formulation is optimized for.
How does stick-slip in way lubrication relate to precision loss in machining?
Stick-slip occurs when the static friction coefficient between the way and the carriage significantly exceeds the kinetic friction coefficient, causing the carriage to momentarily stick, build spring tension in the drive mechanism, then suddenly release and overshoot before sticking again — a cycle that repeats at a frequency determined by the machine's stiffness and feed rate.
On precision grinding, honing and fine-finishing operations, where feed rates are deliberately very low and surface finish tolerances are measured in single-digit microns, even a small stick-slip amplitude translates directly into visible chatter marks or dimensional error on the finished part. This is a way-lubrication problem specifically, addressed through tackifier chemistry and friction-modifier additives in the way oil formulation, and it has no equivalent failure mode in spindle lubrication, where the bearing surfaces are in continuous relative rotation rather than intermittent sliding contact.
Do way lubricants and spindle oils need to be compatible with machine coolant?
Yes, and this is a formulation constraint that applies more visibly to way oils, since way surfaces on most CNC machine tools are directly exposed to coolant splash and mist during machining, while spindle oil circulates in a sealed bearing housing largely isolated from coolant contact. A way oil that emulsifies readily with water-based coolant will contaminate the coolant sump, reduce coolant life, and lose its own tackifying and film-forming performance as it picks up water.
Machine tool builders specify way oils with demulsibility characteristics tested against the coolant types expected in service, and formulators building way lubricants must verify this compatibility rather than assume a generic mineral or synthetic base oil will separate cleanly from every coolant chemistry on the market.
Formulating Precision Machine Tool Lubricants?
Global Formulation provides lubricant consultancy — way oil tackifier systems, spindle oil viscosity and additive selection, coolant compatibility testing, and formulation support across the machine tool lubricant range.
Talk to Our Formulation Team